Wholesale Functional Trainer for CrossFit Boxes | Bulk OEM Guide
Tolerance precision matters far more than the rated load capacity printed on a spec sheet when outfitting a CrossFit box. For bulk procurement, the real cost drivers are not unit prices but the hidden expenses of airfreight replacements and on-site rework caused by poor weight-stack pin tolerances and pulley fatigue failures under high-impact daily use.
I grew up next to Beilun Port in Ningbo and spent my early years assembling strength equipment on factory floors before moving into overseas after-sales and eventually sales. I still remember a full container of cable machines we shipped to a CrossFit affiliate in the Middle East. When the boxes were opened on the warehouse floor, the selectorized pin diameter ran oversized by roughly two millimetres. Nothing slid into the weight stacks. The entire shipment sat in a bonded warehouse for weeks, and the airfreight cost to rush replacement pins wiped out a large chunk of the margin we had built into the order. That single incident changed how I approach every wholesale functional trainer for CrossFit Boxes project: I now scrutinise tolerance control records more aggressively than I negotiate pricing. [NEED_CITE: root cause distribution of field failures in selectorized strength equipment per ISO 20957 series]

The lessons from that container shaped everything that followed. When a box owner asks me to quote a full rig package, my first questions are never about colour or logo placement. I ask how many athletes train per day, what the drop-zone floor loading looks like, and whether the facility runs competitive WODs with repeated barbell and plate impacts. Only after those answers do I start configuring the functional trainer for CrossFit Boxes build.
Why CrossFit Boxes Need Different Functional Trainers Than Commercial Gyms?
A CrossFit box subjects a functional trainer to a fundamentally different stress profile than a traditional commercial gym, demanding structural redundancy far beyond standard fitness equipment norms. In a typical health club, a cable crossover sees controlled, slow-tempo isolation work. In a box, the same style of machine is used for high-rep pull-throughs, banded face-pulls, ring rows anchored to the frame, and occasional accidental plate drops against the base during timed workouts. [NEED_CITE: comparative usage intensity data between functional training affiliates and commercial health clubs]
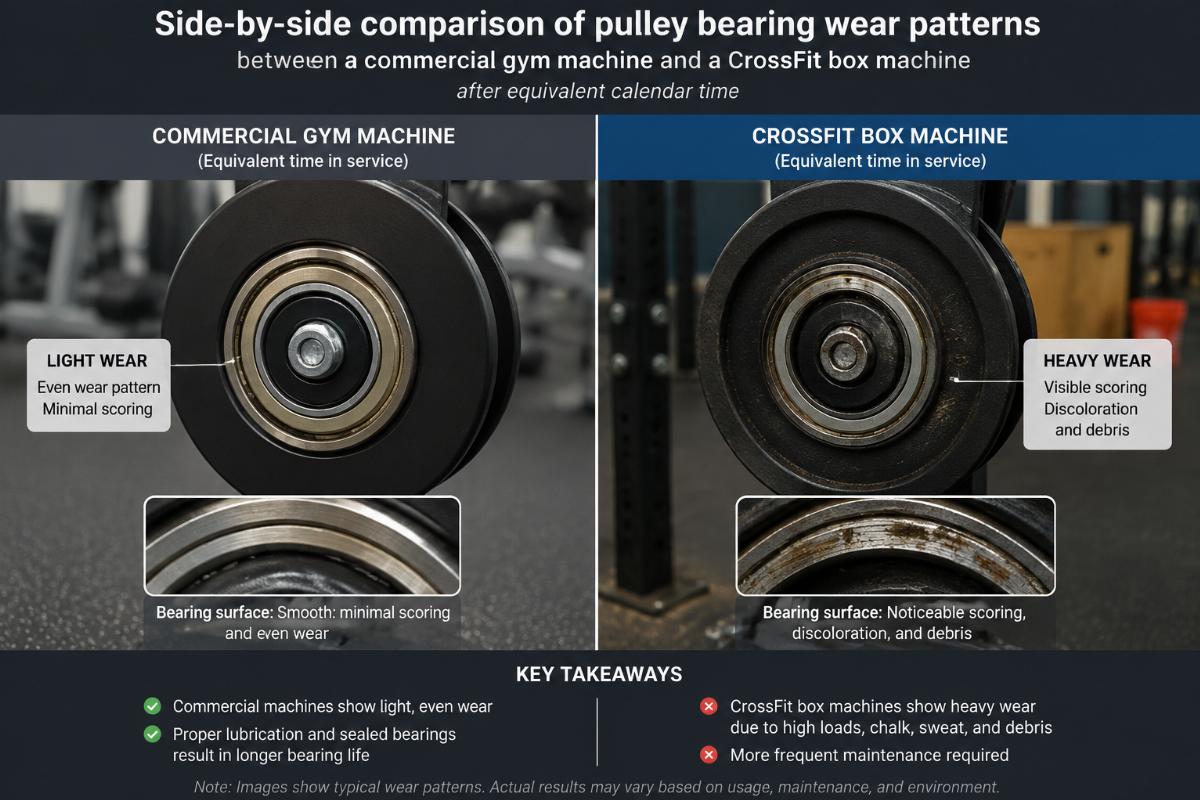
From my time walking affiliate floors during installation trips across Latin America and the Gulf, I have watched machines that would last a decade in a hotel gym show pulley wear and cable fraying within a single season inside a box. The difference is not just volume; it is the shock-loading pattern. Athletes transition between movements with minimal rest, and cables are frequently tensioned and released abruptly rather than guided through smooth eccentric phases.
I once oversaw the commissioning of a multi-station rig for a box in a coastal city in Mexico. Within months, the facility manager reported that the dual adjustable pulley towers were producing audible clicks during crossover drills. On inspection, the pulley bearings had developed play because the sealed cartridge units were never rated for the lateral shock loads generated by athletes kipping into cable attachments. The manufacturer had supplied standard commercial-grade bearings, which are perfectly adequate for a Planet Fitness-style environment but simply do not survive a box. We ended up swapping in higher-load-rated bearings across the entire fleet, and the retrofit cost ran into multiple times the original price differential between the commercial-grade and heavy-duty bearing options.
This is why any serious wholesale functional trainer for CrossFit Boxes specification must start from the usage scenario and work backwards to component selection. [NEED_CITE: bearing load rating methodology per ISO 281 for dynamic shock conditions] The frame tube thickness, the gusset geometry at high-stress junctions, and the pulley shroud design all need to be evaluated against impact frequency rather than static load capacity alone.
What Specs Actually Matter for Bulk Functional Trainer Orders?
Three specification areas dominate real-world durability in a CrossFit environment: selectorized pin tolerance, pulley cable assembly endurance, and base plate load distribution footprint. These are the parameters that determine whether a shipment arrives and stays functional, or whether it becomes a recurring source of warranty claims and member complaints.
Let me walk through each in the order I check them on a factory audit.
Selectorized pin and weight stack bore tolerance. This is the dimension that caused the Middle East container disaster I mentioned earlier. The pin must slide cleanly into every plate without binding, yet without so much play that it rattles and wears the bore oval over time. In a box setting, where athletes grab and release the pin mid-set under fatigue, a sloppy fit accelerates bore elongation and eventually leads to plates jamming at awkward angles. [NEED_CITE: linear fit tolerance classes for selectorized strength equipment per ISO 20957-1]
Pulley cable assembly and wire rope construction. The cable is the single most fatigue-prone component on any functional trainer. In a box, the cable sees not just repetitive cycling but abrupt direction changes and occasional shock loads when an athlete drops a handle mid-rep. The wire rope construction, the number of strands, and the core type all influence fatigue life. I look for cables rated to a breaking strength that substantially exceeds the maximum stack load, with a safety margin that accounts for dynamic shock rather than just static weight. [NEED_CITE: wire rope fatigue testing methodology for fitness equipment per EN 957-1 annex provisions]
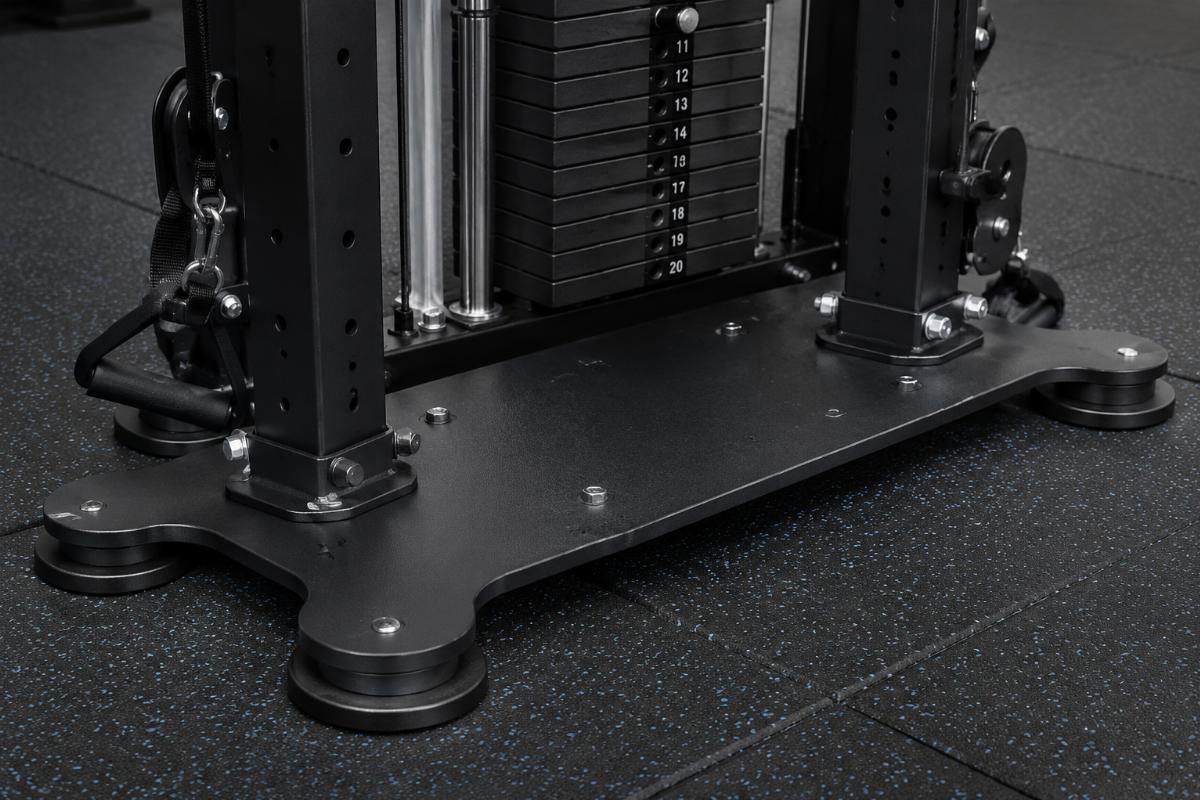
Base plate footprint and load distribution. CrossFit boxes often train on rubber flooring over concrete, and the base plate of a functional trainer must distribute load broadly enough to avoid concentrating stress on a small area, which would crack tiles or indent the rubber over time. A wider base plate with multiple contact points also improves lateral stability during single-arm cable work, reducing the tendency of the unit to shift during heavy pulls.
| Specification Area | Standard Commercial Build | CrossFit-Grade Build |
|---|---|---|
| Selectorized pin tolerance | Self-reported, uncontrolled | Controlled, batch-verified |
| Pulley cable safety margin | Basic | Substantially extended |
| Base plate load distribution | Noticeably narrower | Robust, multi-point contact |
| Frame gusset reinforcement | Minimal | Full junction reinforcement |
| Bearing duty rating | Standard commercial | Heavy-duty shock-rated |
When I review a quotation for a wholesale functional trainer for CrossFit Boxes order, I ask the factory to provide tolerance inspection records for the weight stack pins from at least three recent production batches. If they cannot produce those records, I treat the quote as high-risk regardless of how attractive the unit price looks.
How to Avoid Costly Mistakes in OEM Functional Trainer Procurement?
The most expensive mistake in bulk OEM procurement is selecting a supplier based on catalogue specifications and unit price while neglecting to verify their in-process tolerance control capability on the factory floor. A glossy brochure can list impressive steel thickness and load ratings, but those numbers mean nothing if the welding jigs are misaligned or if the drilling template for the weight stack holes has worn beyond acceptable limits.
I structure my factory audits around three checkpoints that directly map to the failure modes I have seen in the field.
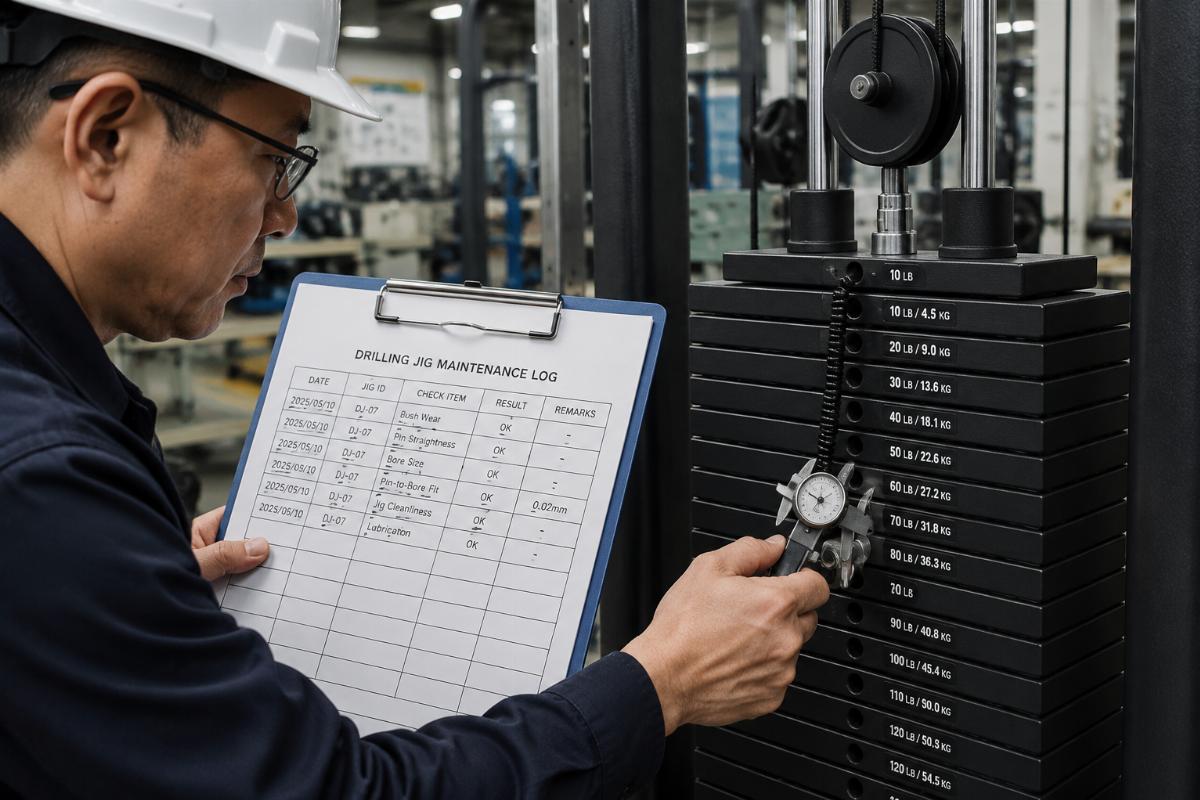
First, inspect the drilling jigs and fixture maintenance logs. The weight stack plate holes and the selectorized pin guide tubes are drilled using dedicated jigs. Over time, these jigs wear, and the hole positions drift. A factory that does not track jig replacement intervals will produce batches where some units are perfect and others have pins that bind on certain plates. During one audit at a manufacturer’s production facilities in the interior, I found that the drilling jig for a popular functional trainer model had not been replaced in several years, and the maintenance log showed no periodic verification. The tolerance scatter on the pin-to-bore fit was visibly wider than what the spec sheet implied.
Second, review the cable assembly process and incoming wire rope inspection. The cable routing path, the swaging method, and the thimble selection all affect long-term fatigue performance. I ask to see the incoming inspection records for the wire rope, specifically the mill test certificates confirming strand count and core type. I also watch the swaging operation to confirm that the dies are changed on schedule and that operators check crimp dimensions with go-no-go gauges. [NEED_CITE: swaging quality inspection criteria for fitness equipment cable assemblies]
Third, evaluate the pre-shipment assembly and function-test protocol. A factory that fully assembles a sample of functional trainers from each batch and runs them through a simulated use cycle will catch tolerance stack-ups and cable routing issues before the goods are crated. A factory that ships knock-down and relies on the buyer’s receiving team to discover problems is transferring risk and cost downstream.
I worked with a distributor in Southeast Asia who had been sourcing cable machines from a factory that skipped full assembly testing. Every container arrived with a handful of units where the cables had been pinched during packaging because the shroud clearance was too tight. The distributor’s local team spent days disassembling and re-routing cables on the receiving dock. Switching to a supplier that performed full pre-shipment assembly testing eliminated the dock rework entirely, and the total landed cost dropped noticeably even though the per-unit FOB price was slightly higher.
What Is the Real Cost of Poor Tolerance Control in Bulk Orders?
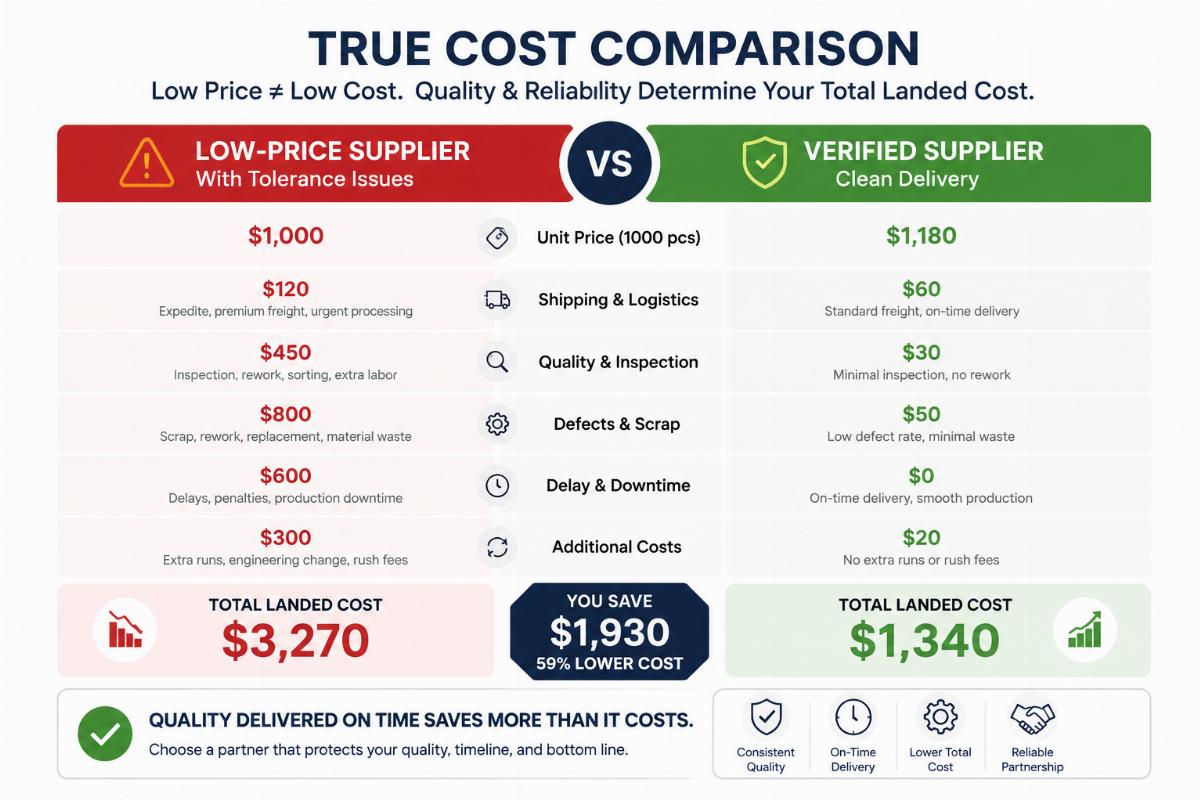
The true cost of poor tolerance control in a bulk order extends far beyond the per-unit price difference and manifests as airfreight replacement expenses, on-site rework labour, and reputational damage with the box owner’s members. These hidden costs routinely dwarf the savings achieved by choosing a marginally cheaper supplier.
Consider the full cost chain when a selectorized pin tolerance issue is discovered after the container has cleared customs at the destination port. The immediate costs include bonded warehouse storage fees, the labour to unpack and inspect every unit, and the decision point: rework on-site or airfreight replacement parts. On-site rework often requires specialised tools and skilled technicians that the local receiving team may not have, particularly for welded frame adjustments. Airfreight replacement parts, while faster, carry freight costs that can run into multiples of the original sea freight allocation per unit.
Beyond the direct financial costs, there is the schedule impact. A CrossFit box that has promised its members a new training area by a certain date cannot simply push the opening back when the equipment is stuck in a warehouse. The box owner faces member complaints, potential refund requests, and lost sign-up revenue during the delay. I have seen box owners absorb a mid-five-figure revenue shortfall because a rig opening was delayed by several weeks due to tolerance-related rework.
The reputational cost is harder to quantify but equally real. In the tight-knit CrossFit community, box owners talk to each other. A distributor who delivers a container of functional trainers that require weeks of remediation will find it difficult to win repeat orders or referrals. Conversely, a distributor who delivers equipment that installs cleanly and performs reliably from day one builds a reputation that generates organic leads across multiple regions.
This is why I always frame the conversation with box owners and distributors around total landed performance cost rather than unit price. A wholesale functional trainer for CrossFit Boxes order that costs slightly more per unit but arrives with verified tolerance records and clean installation performance will always deliver a better return than a cheaper order that triggers a cascade of downstream costs. [NEED_CITE: total cost of ownership methodology for commercial fitness equipment procurement]
Conclusion
Outfitting a CrossFit box with functional trainers requires a procurement approach rooted in usage-scenario engineering rather than catalogue comparison. Tolerance control on selectorized pins, pulley cable endurance under shock loading, and base plate load distribution are the three specifications that determine whether a bulk order performs in the field or becomes a costly remediation project. Verifying a factory’s in-process tolerance management capability before placing an order is the single most effective step a buyer can take to protect margin and reputation.